Before You Strip the Circuit: Verifying Hydraulic Pressure Gauge Readings
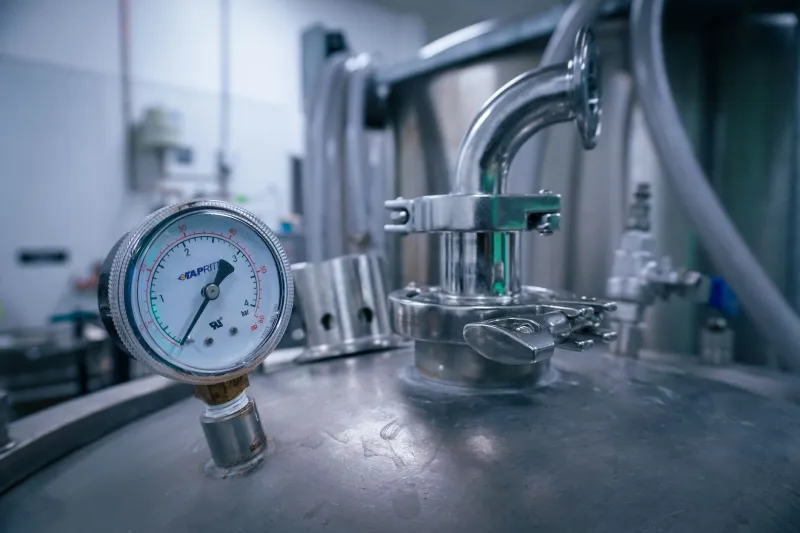
When a hydraulic machine underperforms, the pressure gauge is often the first witness called. A low reading suggests a weak pump; a high reading suggests a restriction; an unstable reading suggests air or a failing component. The trouble is that the gauge is not an independent observer. It is a mechanical instrument connected to the circuit through a small bore line, a snubber and an isolation valve, and any of those elements can mislead an otherwise competent technician.
The gauge is part of the circuit
A pressure gauge is a pressure-measuring device with its own failure modes. Inside a Bourdon tube gauge, a curved tube deflects under pressure and drives a pointer through a linkage. That mechanism can be damaged by overpressure, vibration or corrosion. The gauge line can trap air, the snubber can block, and the isolation valve can be partly closed. The result is not always a dead gauge. More often, it is a gauge that reads plausibly but incorrectly.
That plausibility is the danger. A reading of 120 bar instead of 160 bar looks like a system problem, not an instrument problem. A technician may then test the pump, inspect the relief valve or strip a valve block, all on the basis of a number that was never trustworthy. Before dismantling anything, it is worth proving the reading.
Snubber blockage and sluggish response
Snubbers are fitted to protect gauges from pressure pulsation and shock. They do that by restricting flow into the gauge, which also means they can gradually clog with dirt, sealant debris, corrosion products or oil breakdown residue. A blocked snubber often produces a reading that is slow to rise, slow to fall or lower than the true system pressure. In severe cases, the pointer may barely move even when the circuit is clearly working.
A useful test is to compare the gauge response with a known event. Does the pointer move promptly when a function is operated? Does it settle or creep? If the gauge is sluggish, do not assume the hydraulic system is sluggish. Isolate the gauge line, inspect the snubber and check that the correct restrictor size is fitted. A snubber that has been replaced with an unnecessarily fine restrictor can create the same symptom.
Dry versus glycerine-filled gauges
Glycerine-filled gauges are common in plantrooms and on mobile equipment because the filling damps vibration and protects the movement. They are a sensible choice where pulsation and shock are routine. However, they are not automatically better in every application. A glycerine-filled gauge can be harder to read when the window fogs or the filling darkens, and in cold outdoor locations the filling becomes more viscous. That can affect response, especially on a gauge that is already connected through a restrictive line.
Dry gauges have their place on clean, stable test points and in applications where a fast response matters more than vibration damping. The choice should follow the duty, not habit. If a glycerine-filled gauge is fitted to a test point that is used for setting pressures, confirm that its response is acceptable at the prevailing temperature. Also check for leaks around the fill plug and for contamination of the filling, which can obscure the dial.
Isolation valves and gauge line traps
An isolation valve is there to allow gauge replacement without depressurising the circuit, but it introduces another point of doubt. A valve that is not fully open can restrict flow and produce a low reading. A valve with a damaged seat or a blocked port can do the same. On some installations, the gauge line itself can trap air, particularly where the connection is at a high point or where the line has a poor route.
Do not assume that an open lever means an open passage. Where it is safe and permitted, verify flow through the gauge line using the approved procedure. Check that the correct valve type is fitted and that the gauge connection is not relying on a sealing washer that has partly closed the port. If the gauge reads differently after cracking and re-tightening the connection, the line or valve is suspect.
Calibration drift in UK plant conditions
Calibration drift is not limited to laboratory instruments. Pressure gauges in UK plants face temperature cycling, humidity, vibration and occasional overpressure. A gauge that has been subjected to a pressure spike may read high or low afterwards. Corrosion can stiffen the movement. A pointer can be bent during cleaning or maintenance. The result is a reading that looks stable but is offset from reality.
Calibration intervals should reflect criticality and environment, not just the manufacturer's default. Gauges used for setting relief valves, verifying pump performance or making acceptance decisions deserve particular attention. A gauge used only for coarse indication may need less frequent formal calibration, but it still needs a basic zero and response check.
A short checklist before stripping a circuit
Before removing a pump, valve or actuator, verify the evidence:
- Compare the installed gauge with a calibrated test gauge at a suitable test point. If the two disagree, stop and investigate the instrument path.
- Confirm the isolation valve is fully open and the gauge line is not blocked, kinked or trapped.
- Check the gauge range and units. A 0 to 400 bar gauge is poor for resolving small changes, and bar versus psi confusion remains a common error.
- With the circuit safely depressurised, check that the gauge returns to zero. A pointer that rests above or below zero is a warning.
- Inspect the snubber, connection and gauge window for contamination, leaks, fogging or damage.
- Record the reading, the test gauge reading and the conditions. If the instrument is suspect, replace or recalibrate it before repeating the diagnostic test.
When to replace rather than recalibrate
Not every gauge is worth recalibrating. A gauge with a bent pointer, a damaged case, a leaking glycerine fill, a fogged window or evidence of overpressure should generally be replaced. The cost of a new gauge is small compared with the cost of a misdiagnosis. For critical test points, consider a calibrated digital test gauge or a pressure transducer with a known calibration status.
Gauge blindness is a quiet reliability issue. It does not announce itself with a leak or an alarm, but it can send a maintenance team in the wrong direction. Treating the pressure gauge as a suspect until proven otherwise is not cynicism; it is good diagnostic discipline. Verify the instrument, then trust the circuit.