After the Repair, the Residue: A Flushing Regime for Contaminated Hydraulic Circuits
Photo: hydraulic flushing rig filter cart reservoir maintenance engineer industrial, via pmvishwakarmayojana.com
The assumption that follows a repair
When a pump or valve fails, the immediate priority is to restore production. The failed item is replaced, the reservoir is drained, a new filter is fitted and fresh oil is added. The machine runs, the pressure holds and the job appears complete. Yet a drain and refill is a fluid change, not a cleaning operation. It removes only the oil that will flow to the drain point. It does not remove debris held in low-velocity lines, cooler tubes, accumulator pipework, blind ends or the boundary layer on reservoir walls. Nor does it remove the fine particles suspended in the oil film on internal surfaces. A refill therefore dilutes contamination rather than eliminating it. In a busy UK plant, that dilution can look like a cure until the replacement pump reaches its first few hundred hours.
What a drain leaves behind
Hydraulic systems are not simple tanks. They contain coolers with small passages, long return lines, directional valve galleries, dead legs and reservoir floors that may never see vigorous flow. After a catastrophic failure, the debris burden is varied: metallic flakes from gear or piston surfaces, elastomer fragments from seals, and fine silt from long-term wear. Heavy particles settle in low-flow zones. Light particles remain suspended and migrate when flow resumes. A new filter will capture some of this material, but it will also go on bypass when loaded, and it cannot clean surfaces that the oil never scours.
Set a cleanliness target before choosing a method
A flushing protocol needs acceptance criteria. For most industrial hydraulic systems, the ISO 4406 cleanliness code is the appropriate measure. A typical target for sensitive servo or proportional systems might be -/16/13 or better; for robust industrial circuits, -/18/15 may be acceptable. The target should be based on component tolerance, not habit. If the original equipment manufacturer specifies a code, use it. If not, set a target at least as clean as the most sensitive component requires, and record it on the work order. Decide the sample points in advance: reservoir return, pump inlet, cooler outlet and any known dead leg. A single sample from the reservoir is not proof of circuit cleanliness.
Build the flushing circuit deliberately
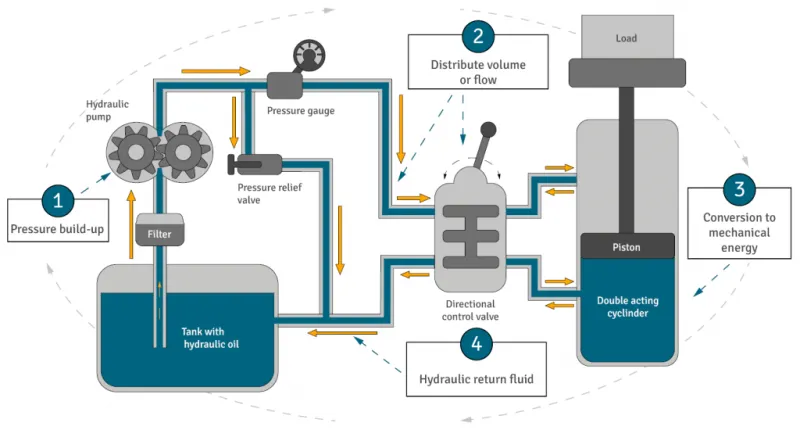
Flushing is a controlled, temporary hydraulic circuit. Where practical, isolate or bypass actuators, servos, proportional valves and accumulators. Remove or protect components that cannot tolerate flushing velocity or contaminated fluid. Use a flushing rig with its own pump, heater and filter if the installed pump is not suitable. If the machine pump is used, verify that it is clean and serviceable. The objective is turbulent flow through every line, not merely circulation. Flow velocity matters: aim for a velocity that scours surfaces without damaging seals. In practice, many lines need a flow rate above normal operating flow, but check pressure drop and hose ratings. Temperature control helps, because warm oil reduces viscosity and improves particle release, but stay within fluid and seal limits.
Select filters and fluid with intent
Use high-efficiency filters. A beta ratio of 200 or better at the target micron rating is a sensible starting point for flushing. Absolute-rated elements are preferred over nominal ratings. Place the filter downstream of the component being cleaned and upstream of sensitive parts. Change elements on differential pressure, not on a fixed calendar. Monitor differential pressure and inspect the element for metal and elastomer debris. Flushing fluid should be compatible with the system. A dedicated flushing oil can be useful, but its residue must be drained completely. If using the system oil, confirm it meets the original specification and do not overheat it. Never use kerosene or solvent unless the component manufacturer permits it and the procedure includes documented removal and a compatible oil charge.
Clean the reservoir as a vessel, not just a sump
The reservoir is often the largest contamination store. Drain it, then clean accessible surfaces with lint-free wipes and a compatible cleaner. Remove sludge from corners and the suction strainer area. Inspect breathers, filler caps and air vents. If the reservoir has a sloped floor and drain port, confirm the drain is not blocked by sludge. For welded reservoirs, look for internal baffles that create dead zones. A magnetic rod can help collect ferrous debris, but it is not a substitute for cleaning. After cleaning, carry out a wipe test on the floor and walls.
Verify by sampling, not by appearance
Verification is the step most often skipped. After flushing, circulate the oil, then sample from the agreed points using clean bottles and a consistent method. Take samples with the system at operating temperature and with flow conditions representative of normal running. If the laboratory reports ISO 4406 codes, compare them with the target. A single passing sample is not enough: take a second sample after a short run-in period to confirm that the count is stable. If the code rises, debris is still being released. Continue flushing or investigate the source. Record the results in the asset history so that the next repair starts with evidence.
A short case study
A West Midlands manufacturer replaced a failed pressure-compensated pump on a hydraulic press. The maintenance team drained the reservoir, changed the return filter and refilled with new oil. Within three weeks the replacement pump showed rising case-drain flow and abnormal noise. An oil sample returned an ISO code well above the target, with ferrous particles and elastomer fragments. Rather than replace the pump again, the team flushed the circuit. They bypassed the press cylinders, isolated the accumulator, cleaned the reservoir and installed a high-efficiency off-line filter. They circulated warm oil through the cooler and return lines, changed filter elements on differential pressure, and sampled from the reservoir, cooler outlet and a dead leg. The final sample met the target, and a second sample after two weeks remained stable. In the following quarter, case-drain flow was normal and no further failure occurred. The cost of the flush was a fraction of a second pump replacement and the associated lost production.
Practical close-out
A post-repair flush is not a luxury for fastidious plants. It is the difference between replacing a component and restoring a system. At Newport Fluid Power, the message is simple: a repair restores the component, but a flush restores the circuit. Treat drain and refill as a fluid change, not a cleaning operation. Set the target, flush the whole circuit, verify with samples, and record the evidence.